Posts

Showing posts with the label SRB tube

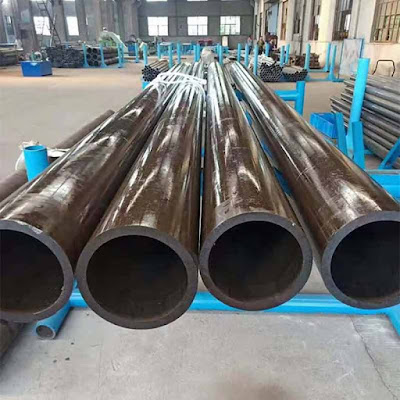
Process of high precision cold drawn tube
Image
  High precision cold drawn tube is a new high-tech energy-saving product. In recent years, using this technology to produce precision steel tube has been widely used in domestic hydraulic, pneumatic cylinder, coal mine support (prop), oil pump pipe, Jack and other manufacturing fields. Precision cold-drawn steel pipes with high precision promote the use of steel, improve processing efficiency, save energy, reduce investment in hydraulic cylinders and cylinder processing equipment is important. Cold drawing method: Comparing with the traditional cutting technology, the production of high precision cold drawing pipe-hydraulic cylinder has the following characteristics: (1) High production efficiency: The traditional method of producing cylinders with diameter of 420 mm and length of 12 meters is 154 hours, and the cold drawing method only takes 4 minutes to produce. (2) Real high speed: Boring of the boring head and play a guiding role in the cutting process, billet tube due to se...

Production process of ST52 chrome plated honed tube

Image
ST52 chrome plated honed tube  is used for the production of mechanical parts. Its precision requirements are high, so it must be said that complicated process and strict inspection can be delivered, and with the continuous development of technology, the production process of honing pipe is constantly improving. perfect. In order to make the production efficiency of ST52 electroplating honing pipe high, we have adopted a new production process, which is produced by grinding and automatic grinding. Among them, automated grinding includes the use of electric or ultrasonic grinding to complete production tasks. The daily working principle of the ST52 electroplating honing pipe is mainly the pressure generated by the sand on the belt, and the surface grinding under the rotation speed. After the upper and lower movement of the abrasive belt, the upper and lower surfaces of the workpiece are grounded back and forth to achieve the effect. Of course, in the grinding process, it is...

The production process of honed tube

Image
While producing honed tubes , our factory uses the honing process to make smooth surface finishes of inside diameters; and to maintain exact tolerances on inside diameters. Under the honing process, abrasive stones and paper are used to the ID of the tubes, which “grinds” stock away to remove surface imperfections from the cold drawing process; and to achieve the desired dimensional tolerances and surface finish. And normally we use cutting fluids to provide easy cutting action and also to remove the cut material from the bore. Honing is a decrease velocity abrading process compared to grinding. Since less pressure and heat is made, the surface, precision and size of the finished product isn’t affected by heat stress. Precision cylinder tubes comprise excellent surface integrity and finish, high accuracy inner diameter tolerances. And an over all dimensions and geometry control that can not be achieved in faster cutting speeds. Anbao Hydraulic has been supplying honed tubes for...

The Difference Between Skiving &Roller Burnishing Tube And Honing Tube

Image
Skiving and roller burnishing process provide high quality hydraulic cylinders with final sizing and creates the desired finish pattern on the interior of tubing or cylinder bores. They are used in the manufacturing of hydraulic cylinders. Compared to honing process, they are 80-90% saving of machine time which reduces tool costs per meter of tube length and produces super finish surface, with a bore tolerance of IT8, thereby reduces the sealing wear making it ideal for pistons. The skiving tool is a multifunctional tool used in the manufacturing of hydraulic cylinders. Skiving is operated like this: Two thin chips are cut at a high feed rate (1-4 mm/rev) while the tool passes through the work piece. This cutting operation determines the finished diameter and tolerance of the hydraulic tube. Surface finish Ra= 4-10 μm (skiving) Skiving has obvious advantages compared with honing: • 80-90% saving of machine time which reduces tool costs per meter of tube length. • Produces su...